
Mold Tooling Design
Plastic Mould Ejection
Plastic mould ejection systems push solidified thermoplastic parts off the mold core after cooling shrinkage locks the resin onto the steel. Selecting the right mechanism—pins, sleeves, blades, valve ejectors, stripper plates, or air valves—prevents part distortion, stress cracking, and surface witness marks.
- Core Clinging Mechanism: Cooling shrinkage reduces plastic volume and forces molded parts to grip the mold core tightly.
- Surface Finish Direction: Grind and polish cavity and core walls with an oilstone parallel to the draw direction so microscopic grooves do not trap pressurized melt.
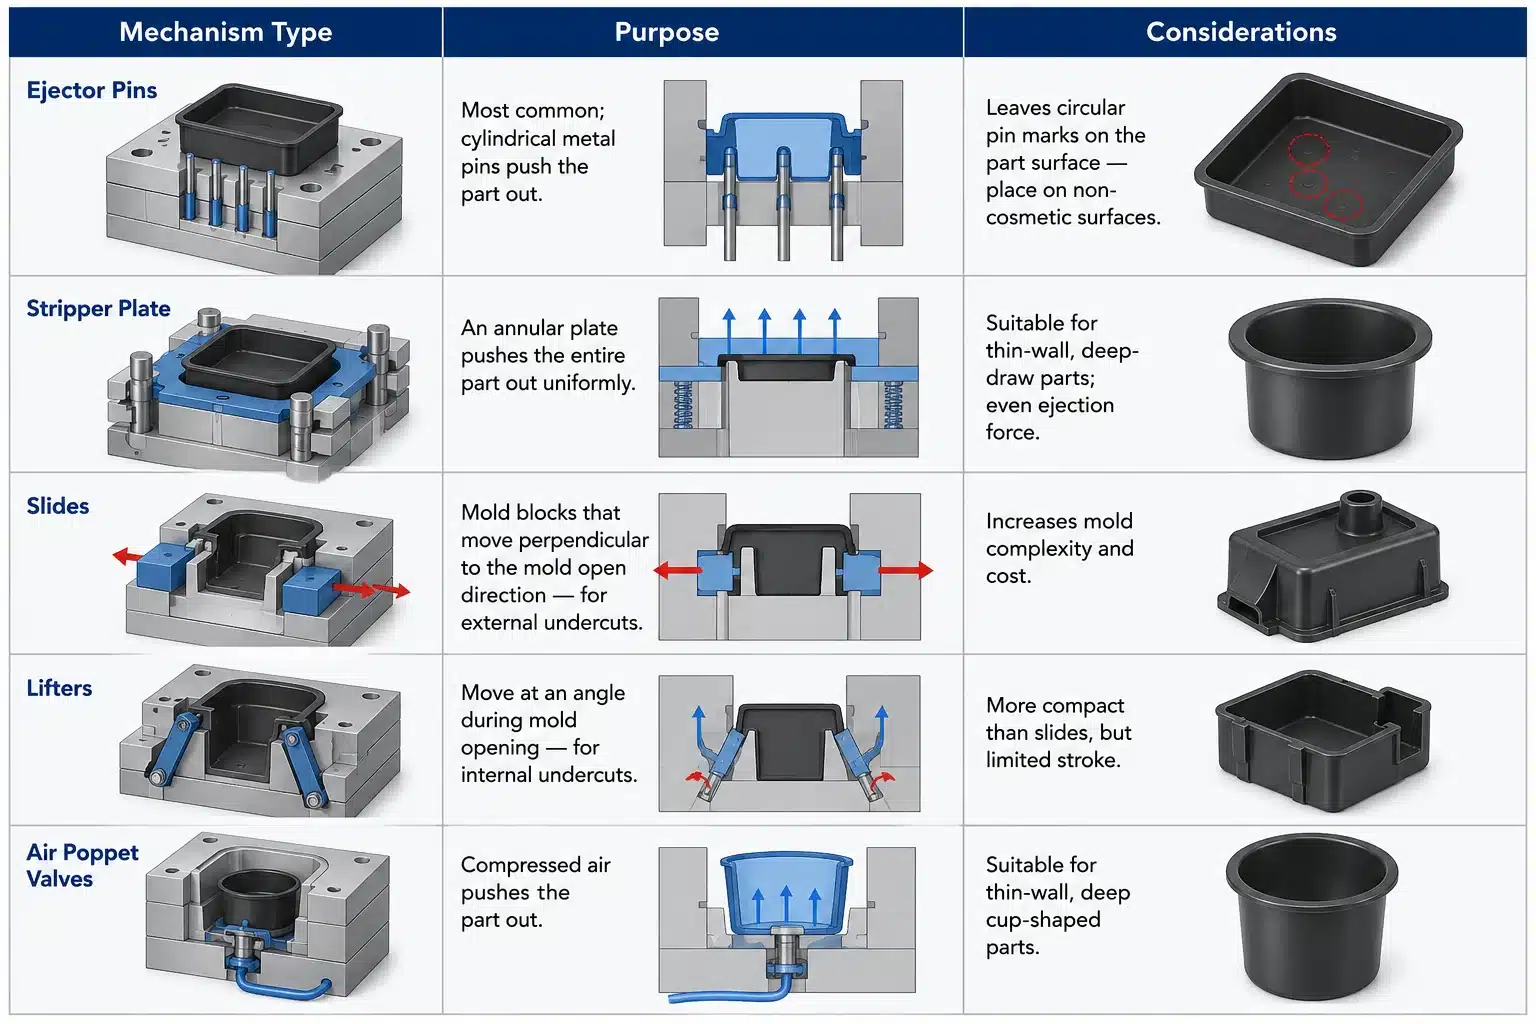
- 5 Primary Ejection Methods: Ejector pins and blades (lowest cost, point load), ejector sleeves (bosses and holes, 2x venting efficiency), valve ejectors (wide flat contact for flexible closures), stripper rings/plates (360° peripheral contact), and pneumatic air ejection.
- Machine Matching: Verify press daylight, ejector cylinder stroke length, and hydraulic core-pulling circuits before finalizing tooling layouts.
Injection moulding compounds contract during cooling, meaning their solid volume is smaller than their molten volume inside the heated barrel. Toolmakers build shrinkage allowances directly into the cavity dimensions to hold tight part tolerances.
Ejection System Design Guide – Pins, Blades, Sleeves & Stripper Plates
Pick an ejector type, then hover or tap any part or number.
| Ejector Pin | Blade Ejector | Ejector Sleeve | Stripper Plate | |
|---|---|---|---|---|
| Use for | Most parts: flat areas, walls, ribs, corners | Thin deep ribs, narrow walls | Bosses, round cores, holes | Round thin-walled cups, caps, containers |
| Push area | Small round spot | Long narrow strip | Full ring around a boss | Whole rim of the part |
| Marks | Round witness marks | Thin line marks on rib ends | Ring mark on boss end | None on the cosmetic surface |
| Cost | Lowest, standard catalog parts | Higher, needs EDM slot | Medium, needs fixed core pin | Highest, extra plate and fits |
| Watch out | Small pins bend; high local stress | Fragile blade section | Thin sleeve walls wear | Mostly limited to round parts |
Shrinkage also forces the cooled plastic part to clamp tightly onto the mold core before ejection begins.
Releasing finished parts without damage requires two primary tooling measures: thorough polishing of all melt-contact surfaces and sufficient draft angles along the direction of draw.
Most thermoplastics provide zero self-lubrication against mold steel. Opening the mold or pushing out hard, rigid resins without proper draft causes drag marks, scratches, and stress cracks.
Buffing hardened tool steel to a simple mirror finish is not enough; toolmakers must grind and polish the areas in the direction of ejection using an oilstone to eliminate transverse scratches and indentations.
High injection pressure forces molten plastic into every microscopic scratch on the core wall, creating mechanical interlocks that block smooth part release.
Directional draw polishing consumes a substantial share of total mold manufacturing time.
The function of an ejection system is to remove the moulded component from the mould once solidified.
Ejection mechanisms differ in stroke geometry, contact area, and actuation cost. Engineers select a specific ejection method based on three core factors:
- Design of component to be ejected;
- Aesthetic considerations of the component;
- Production requirements.
Component designers and toolmakers must align on the ejection layout early in the DFM phase to avoid witness marks on cosmetic surfaces.
Considerations for Ejection Method
Evaluating part geometry, cosmetic surfaces, and press capabilities before selecting an ejection method prevents stuck parts and tool damage during T1 trials. Review this engineering checklist before locking down the mold base layout:
(a) Component aesthetics.
(i) Can ejector pin marks be tolerated on visual presentation faces? Reversing the cavity within the mould design is a proven practice to keep pin witness marks off the cosmetic side.
(ii) Does sufficient draft angle exist on the mould cavity walls to avoid component scuffing or dragging during ejection? Adequate drafting of any moulded component is required and must be built into the 3D part design before tooling begins.
(b) Component dimensional considerations.
(i) What amount of ejection-induced distortion can be tolerated dimensionally? Moulded components distort easily during ejection if unsupported, especially in the case of thin-walled mouldings.
(ii) Will additional ribs be required to stiffen the wall and provide landing pads so ejection takes place without distortion?
(c) Machine considerations.
(i) Is the ejection force sufficient to eject the component within the working limitations of the moulding machine? Designing a deep-draw mould without calculating stripping force requirements leads to stalled cycles and stuck parts.
(ii) Is the intended moulding machine able to actuate the designed ejection system incorporated into the mould design? Machine designs vary in ejection actuation geometry. Most moulding machines actuate ejection along the centre line of the platens in line with the injection unit.
A smaller group of presses actuates via crosshead plungers or puller plates; large-tonnage machines employ cross-headed assemblies to distribute stripping forces evenly across the ejector plate.
(iii) Will additional “core pulling” or actuation circuits be required? Complicated mould designs with external or internal undercuts require multi-core pulling sequences. The moulding machine must provide auxiliary hydraulic core-pulling circuits and programmable sequence controls.
(iv) With the moulding machine and mould combination fully open, does sufficient “daylight” (open platen clearance) exist to allow for component ejection and drop clearance? Insufficient daylight forces the shop to mount the mould in a larger, more expensive machine with a longer opening stroke. Running a small mould in an oversized machine creates four production problems:
- Material degradation caused by longer barrel residence times, plus accelerated mould wear from excessive clamping pressures;
- Component flashing created by platen rocking during closure against the small projected area of the mould;
- Shot-to-shot weight inconsistency caused by a large-volume injection unit metering a tiny shot volume;
- Increased cycle times because larger machine platens travel more slowly than smaller presses.
(v) Is the required ejection stroke within the capability of the moulding machine? Mouldings with deep draw depths, such as tubular housings, require long ejection strokes to clear the core completely.
The maximum available ejection stroke on the moulding machine is fixed by the length of the ejector cylinder (the swept volume of the piston on actuation). The mould designer must verify the press stroke specification before finalizing core height.
(d) Plastic Mold/tooling considerations
(i) Is the ejection system used for cavity venting? Ejector pins and flat blades are routinely placed at the end of fill paths to vent gas traps where blind spots occur inside the cavity.
(ii) Must the ejection system release interfacial vacuums between the component and the mould core before push-out begins? Large thin-walled mouldings, such as container lids, shrink tightly over the core on mould opening and trap a vacuum underneath the part during ejection.
Thin-walled brittle mouldings crack or puncture under vacuum holding forces if the core interface is not vented first.
(iii) Sliding ejection components such as pins and blades induce friction and wear against mould core bores during service, requiring hardened or nitrided guide surfaces.
Plastic Mold Ejection Methods
Five primary plastic mold ejection methods handle part release across standard structural components, cylindrical bosses, and deep-draw thin-wall packaging. The engineering comparison table below summarizes contact geometry, venting performance, and tooling trade-offs for each mechanism:
| Ejection Method | Contact Area & Geometry | Best Part Applications | Venting & Tooling Trade-Offs |
|---|---|---|---|
| Pins & Blades | Small circular point or thin rectangular edge | Standard structural walls, rib bases, non-cosmetic faces | Lowest cost; standard catalog sizes; high point load risks stress whitening on thin walls |
| Ejector Sleeves | 360° annular ring around a stationary core pin | Cylindrical bosses, cored holes, small round gears | Doubles venting clearance vs. standard pins; higher machining cost; wears on both ID and OD faces |
| Valve Ejectors | Wide flat poppet head | HDPE bottle caps, flexible closures, thin flat panels | Large load-bearing area prevents distortion; forms internal seal undercuts; can return via gravity |
| Stripper Ring / Plate | Full 360° peripheral contact along part rim | Deep-draw round containers, buckets, optical bezels | Eliminates pin marks; even stripping force; higher wear on guide bushings and core locators |
| Air (Pneumatic) Ejection | Compressed air pulse through core micro-valves | Large thin-walled lids, elastomeric gaskets, seals, diaphragms | Breaks core vacuum instantly; zero mechanical punch marks; often paired with mechanical plates |
Pins and blades ejection
Ejector pins provide the most economical form of mechanical part release, though their small cross-sectional area concentrates high single-point loads onto the plastic wall during push-out.
Point loading can indent, stress-whiten, or distort the part around the pin tip, particularly on thin-walled mouldings or brittle resins.
Toolmakers fit round ejector pins and rectangular ejector blades (for narrow ribs) using off-the-shelf metric and imperial catalog standards to keep maintenance simple.
Ejector sleeves
Ejector sleeves fit telescopically over a stationary core pin to push out cylindrical features such as bosses, recessed mounting holes, and tubular hubs.
Small circular components can be stripped cleanly using a single ejector sleeve around their outer perimeter. Sleeves cost more to machine than solid pins and experience faster wear because sliding contact occurs on both their internal bore and external diameter.
The annular ring distributes stripping forces evenly around the boss wall while doubling the perimeter venting clearance compared to a solid pin.

Valve ejectors
Valve ejectors use a wide, flat poppet head seated flush inside the mold core to maximize contact surface area during actuation.
The enlarged head spreads stripping pressure across thin-walled panels so the part releases without local buckling or puncture.
Soft, flexible polymers—such as HDPE bottle caps and closures—frequently use valve ejectors to form internal sealing undercuts and strip the part in one stroke. In vertical injection or compression moulds, floating valve ejectors can rely on gravity to drop back into their seat after actuation.
Stripper ring and plate ejection
Interactive Tooling Diagram: Inspect the mold assembly below to see how the stripper plate and ejector assembly align with the core and cavity plates:
Main components of a plastic injection mold
- Core and Cavity — form the shape of the plastic part.
- Runner System — guides molten plastic into the cavity.
- Gate — entry point where plastic flows into the part.
- Cooling Channels — cool the plastic quickly and evenly.
- Ejector Pins — push the finished part out of the mold.
- Slider or Lifter — release side holes and undercuts.
Stripper rings and stripper plates push components off the mould core by applying continuous 360-degree contact around the base perimeter of the part.
Peripheral stripping supports the entire part rim simultaneously, eliminating ejector pin marks and preventing warping on thin-wall containers or deep cylindrical shells.
Because the heavy ring or plate rides on guide bushings and core locators during every cycle, toolmakers must use hardened wear plates and precision alignment locks to prevent galling.
Air ejection

Pneumatic air ejection pairs micro-valves in the core face with mechanical pins or stripper plates to break vacuum seals and blow parts clear of the steel.
Thermoplastic and elastomer molders rely on air-assisted ejection for flexible gaskets, seals, diaphragms, and large thin-walled bins where mechanical pins alone would tear or deform the resin.

Dealing with ejector pin marks, vacuum sticking, or warped thin-wall parts? Send us your 3D CAD model for a DFM and ejection layout review.

