
DFM & Part Geometry
Undercuts and Draft Angles in Injection Molded Part Design
Every injection molded component must release cleanly from the rigid steel cavity and core once the cooling cycle ends. Designing proper draft angles along vertical walls and minimizing mechanical undercuts lowers mold tooling cost, shortens cycle time, and prevents drag marks during part ejection.
- Undercut Cost Impact: Features that block straight-pull ejection require split cavities, hydraulic sliders, or removable inserts—increasing both tooling cost and cycle time.
- Internal vs. External Undercuts: External undercuts release via side-action sliders or split chase blocks; internal undercuts lock onto the core plug and should be redesigned out whenever possible.
- Draft Taper Benchmarks: A 4 in. deep part with a 4° taper yields 0.2796 in. per side (0.0699 in./in.), whereas deep-draw housings (6 to 24 in. deep) can run tapers under 1° (down to 0.001 in./in.).
Undercuts
Modern injection molding practice relies on core principles of design that allow unrestricted part release along the line of draw. The most fundamental rule is that the solidified plastic piece must eject directly from the mold cavity without mechanical interference.
Product designers frequently introduce recessed snaps, side holes, or lip overhangs that create undercuts perpendicular to the mold opening direction, making straight-pull ejection impossible.
When functional undercuts cannot be eliminated, the toolmaker must build split molds, angle-pin sliders, or removable mold inserts—all of which increase upfront tooling cost and piece-part cycle expense.
Avoid undercuts in part CAD unless the mechanical assembly or functional latch design leaves no straight-pull alternative.
External Undercuts

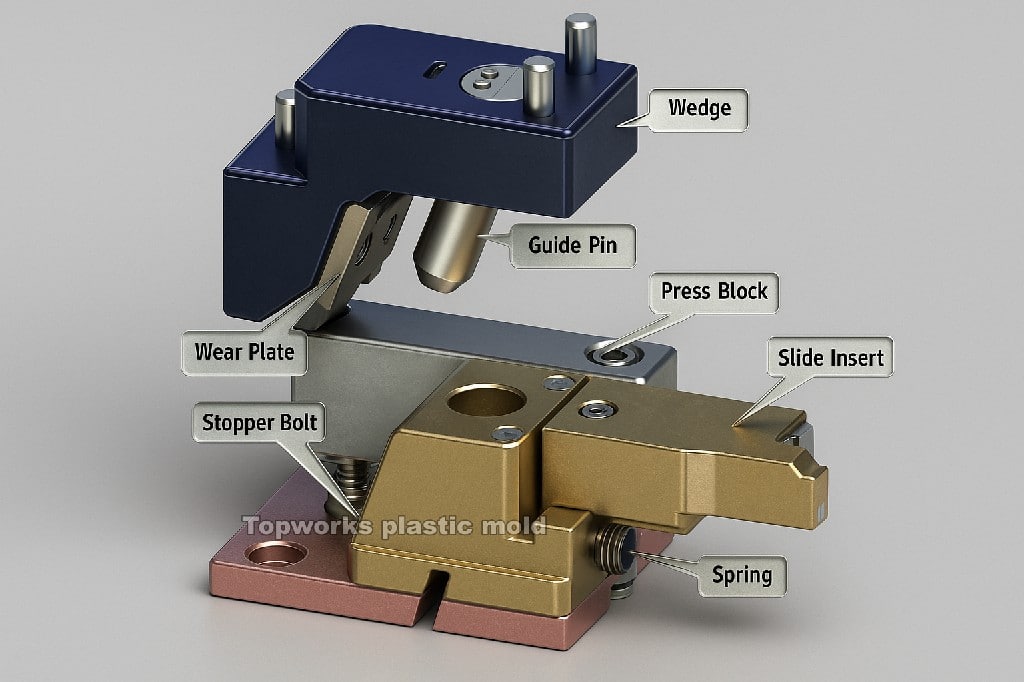
When undercuts sit on the outer perimeter or exterior walls of the component, they are classified as external undercuts. A part with an exterior recess cannot withdraw from a solid one-piece cavity block.
To mold external undercuts, toolmakers split the cavity into two or more movable slider segments or loose split members retained tightly inside a tapered chase block during injection.
Once the plastic solidifies, the mold opens, the sliding members retract laterally to clear the overhang, and the part ejects. Because the cavity is split into separate steel blocks, a visible witness or flash line along the slider seam is unavoidable.
Internal Undercuts
When recessed undercuts sit on the interior walls of a hollow part, they are classified as internal undercuts. While the outer cavity can pull away cleanly on mold opening, the part remains locked onto the internal core plug.
Releasing internal undercuts requires complex collapsible cores or angled lifters; where internal clearance is tight, internal undercuts become impractical to tool and should be eliminated through part redesign (such as adding through-holes for shut-offs).
Taper or Draft
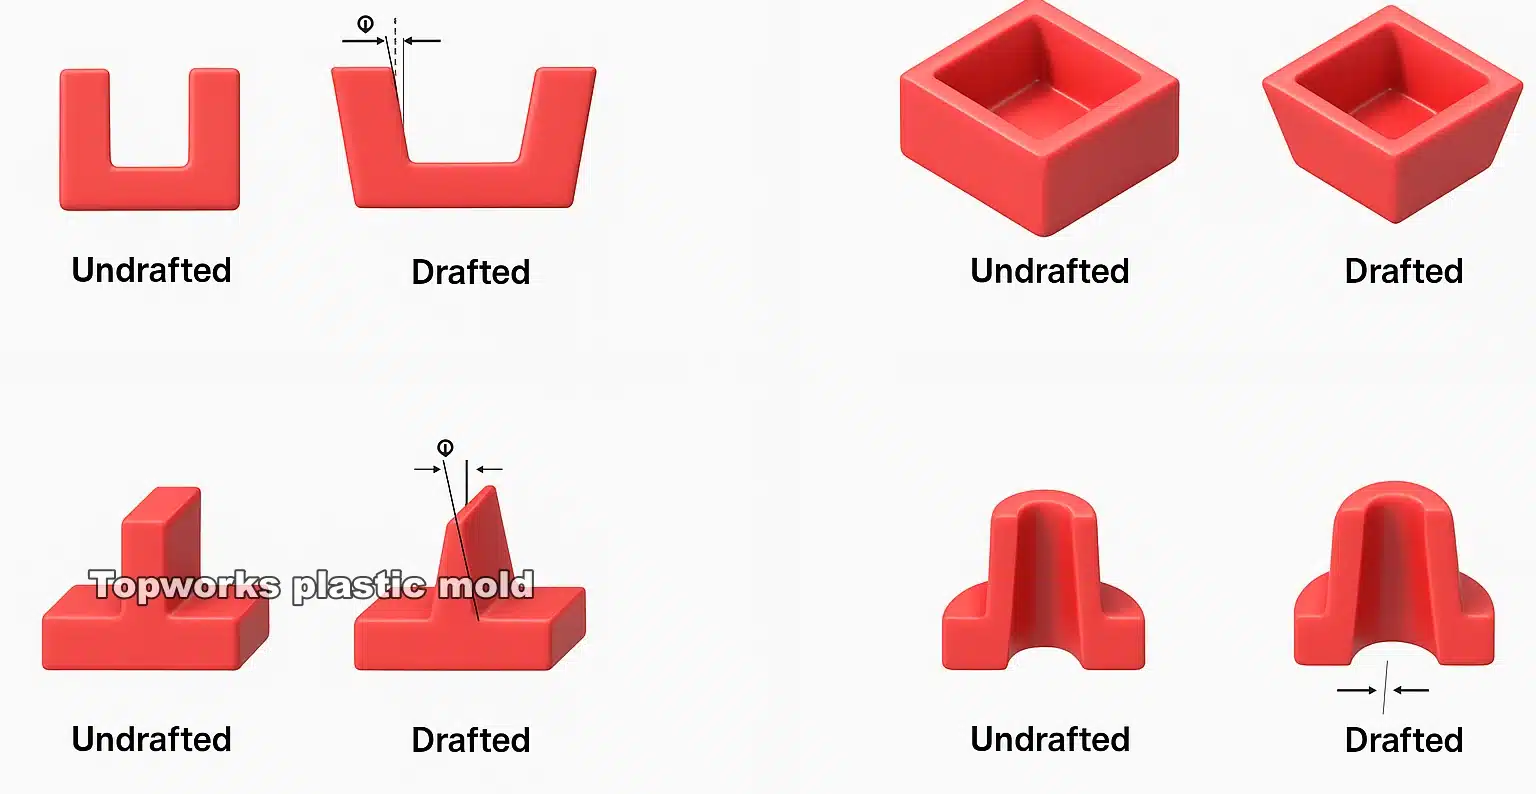
Designing parts from rigid thermoplastics or elastomeric resins requires applying a draft angle (taper) to all vertical walls, ribs, and bosses parallel to the mold draw direction.
Apply draft to both interior core walls and exterior cavity walls, and pair that taper with directional high-luster surface polishing along the vertical faces.
Zero-draft vertical walls create high friction and vacuum lock during mold opening, requiring excessive stripping force that distorts the part. Even a slight taper allows the part to break free from the steel the moment the ejector pins move forward.
In deep-drawn components, converging tapers also create a beneficial wedging action as the mold closes; in compression molding of thermosetting resins, this wedging action increases material density in the upper wall sections.
| Part Draw Depth | Draft Angle / Taper Rate | Total Offset Per Side | Typical Molding Application |
|---|---|---|---|
| 4 in. depth | 4° taper (0.0699 in./in.) | 0.2796 in. per side | Shallow structural housings allowing generous wall taper |
| 10 in. depth | 4° taper (0.0699 in./in.) | 0.6990 in. per side | Theoretical offset (often too wide for deep functional walls) |
| 6 to 24 in. depth | < 1° taper (down to 0.001 in./in.) | 0.006 to 0.024 in. per side | Deep-draw radio, television, and appliance enclosure side walls |
Required draft angle varies with draw depth. While engineers should specify the most generous taper the assembly allows, deep-draw parts cannot tolerate a 4-degree taper (which shifts the wall by 0.2796 in. per side at 4 inches deep, or 0.6990 in. per side at 10 inches deep).

Production molding proves that deep enclosures—such as cabinet side walls 6 to 24 inches deep—release reliably with tapers under 1 degree (as small as 0.001 in. per in.) when paired with draw-polished steel.
Combining proper wall draft with rounded corners, generous internal fillets, and domed surfaces improves melt flow, part appearance, and ejection reliability across injection, transfer, and compression molds.
Unsure if your part’s undercuts or draft angles are ready for tooling? Send us your 3D CAD file for a free manufacturability check.

