
Defect Troubleshooting
Flash Lines in Injection Molding: Root Causes and Tooling Fixes
Flash in injection molding is a thin wafer of excess molten plastic that escapes cavity boundaries along the parting line, ejector pin bores, or slider shut-offs. Eliminating flash lines requires matching press clamping tonnage to cavity pressure and maintaining tight steel-to-steel shut-off tolerances.
- Parting Line Steel Fit: Gaps or insufficient preload between core and cavity shut-offs allow pressurized melt to extrude outside the part perimeter.
- Process Pressure Spikes: Excessive injection pressure, high barrel melt temperature, or late velocity-to-pressure (V/P) transfer forces resin into micro-seams.
- Press Platen Calibration: Out-of-parallel platens or worn tie-bars reduce effective clamp lock across the mold face.
- Corrective Sequence: Audit steel shut-off spotting first, verify clamping force against projected area, then step down packing pressure and melt temperature.

Flash appears along parting seams, movable core inserts, and ejector sleeves whenever internal cavity pressure overcomes the mechanical clamping force holding the steel closed. Left uncorrected, flash ruins part cosmetics, requires costly manual deflashing, and crushes hardened parting-line steel during mold closure.
| Root Cause Category | Primary Failure Mechanism | Corrective Engineering Action |
|---|---|---|
| Poor Mold Design | Weak support pillars, excessive clearance on sliders/pins, or poor parting line spotting | Re-spot shut-off surfaces, add support pillars to stop platen deflection, tighten sliding fits |
| Process Parameters | Excessive injection/packing pressure, overheated low-viscosity melt, or slow fill freeze-off | Lower barrel and nozzle temperatures, reduce pack pressure, optimize V/P switchover point |
| Faulty Equipment | Platen parallelism drift, worn tie-bar bushings, or uncalibrated hydraulic pressure valves | Level and calibrate press platens, inspect tie-bar stretch, replace worn barrel check rings |
Poor Design
Inadequate mold structural support and loose component clearances are primary mechanical causes of parting-line flash. If the mold base lacks sufficient support pillars behind the cavity plate, high injection pressure bends the steel platen backward and opens a gap along the parting line.
High-viscosity resins require elevated injection pressures to fill thin walls; if moving sliders, lifters, or ejector pins carry excessive machining clearance, pressurized plastic extrudes directly into those seams.
Incorrect Processing Parameters
Over-pressurizing or overheating the polymer melt forces plastic past intact mold shut-offs. Excessive barrel temperatures drop melt viscosity, allowing fluid resin to penetrate microscopic venting channels and parting seams.
Conversely, running an overly slow injection speed cools the melt front prematurely inside thin sections; the machine then spikes hydraulic pressure to force the remaining shot into the cavity, blowing open the parting line near the gate.
Faulty Equipment
Uncalibrated clamping units and worn injection barrels generate flash even on a well-built mold. When press platens lose parallelism or hydraulic clamp valves drift out of calibration, clamping tonnage distributes unevenly across the mold face.
Addressing flash requires isolating whether the defect stems from steel wear, process settings, or press mechanics:
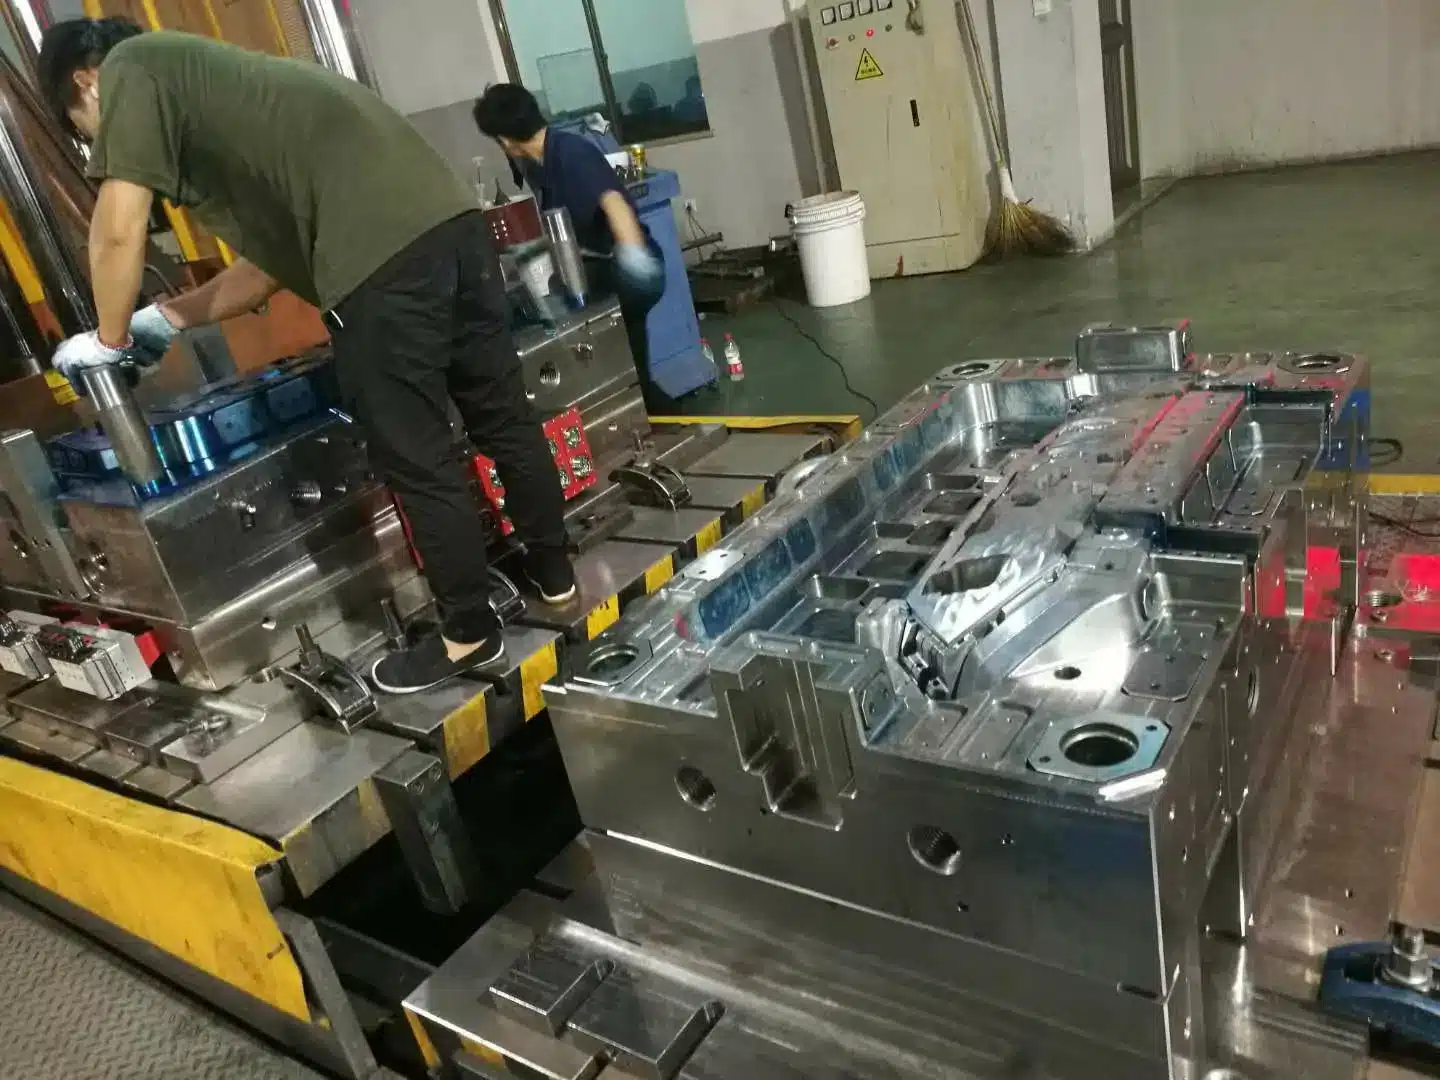
- Tooling Remediation: Perform a blue-ink spotting check on the parting line, grind support blocks to restore preload, and replace worn ejector pins or slider wear plates.
- Process Tuning: Lower injection and holding pressures incrementally, verify melt temperature with a pyrometer, and match nozzle orifice size to the sprue bushing.
- Press Maintenance: Calibrate hydraulic pressure transducers, verify tie-bar tonnage balance, and maintain consistent process control discipline across shifts.
Takeaway
Eliminating flash in injection molding protects both part tolerances and mold steel longevity. By combining rigid mold base support, precision parting-line spotting, calibrated platen tonnage, and balanced packing pressures, molders prevent excess resin extrusion without starving the cavity.
Struggling with parting line flash or slider shut-off wear on an existing tool? Talk to our tooling engineers for a mold design and process audit.

